Client
Sector
BONNER Provided

The Challenge
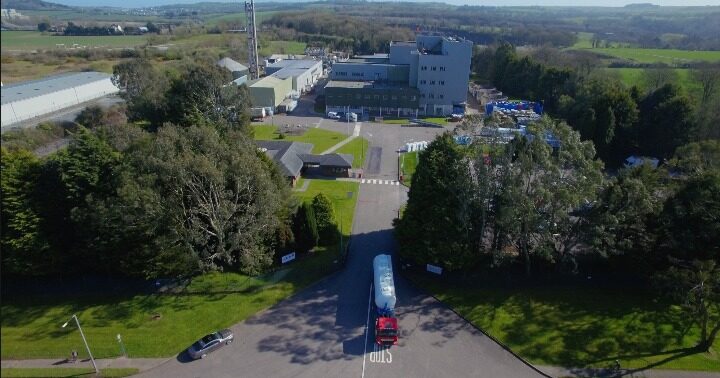
Carbon Group operates a chemical manufacturing site in Ringaskiddy, County Cork, where processes are hazardous and tightly regulated, including ATEX areas and strict environmental controls.
Since 2019, BONNER has delivered at least one automation project on the site every year. What began as an established service relationship has developed into a long-term automation partnership, with BONNER supporting Carbon Group across control systems, functional safety and plant-wide data acquisition.Each project has built on the last, allowing BONNER to develop a detailed understanding of the site, its processes and its engineering requirements. Today, Carbon Group turns to BONNER as a trusted automation partner for ongoing projects and system development.
Carbon Group needed an automation partner that understood the complexities of its site and could deliver projects from concept and design through to build, installation and commissioning.
Working within a live chemical manufacturing environment meant reliability, safety and minimal disruption to production were essential. Carbon Group also wanted to retain the involvement of its own engineering and maintenance teams throughout each implementation. The requirement was therefore for more than an equipment supplier, it needed a specialist automation partner that could work alongside its team and develop solutions around the needs of the plant.
Operational Impact
BONNER’s automation team has delivered a series of projects that have progressively extended the site’s automation and monitoring capabilities.The work has included pressure monitoring for volatile gas storage, automated wastewater monitoring and dosing, a plant-wide SCADA system, energy monitoring, secure remote access and functional safety systems.
As Carbon Group’s requirements evolved, BONNER continued to build on the existing infrastructure, integrating additional instrumentation, expanding SCADA functionality and rationalising alarms.
Pressure Monitoring for Volatile Gas StorageBONNER designed, built, installed and commissioned a pressure monitoring system for volatile gas storage within an ATEX zone.The system monitors pressure and provides local and remote visual and audible alarms for low-pressure and fault conditions, while distinguishing new alarms from standing alarms.
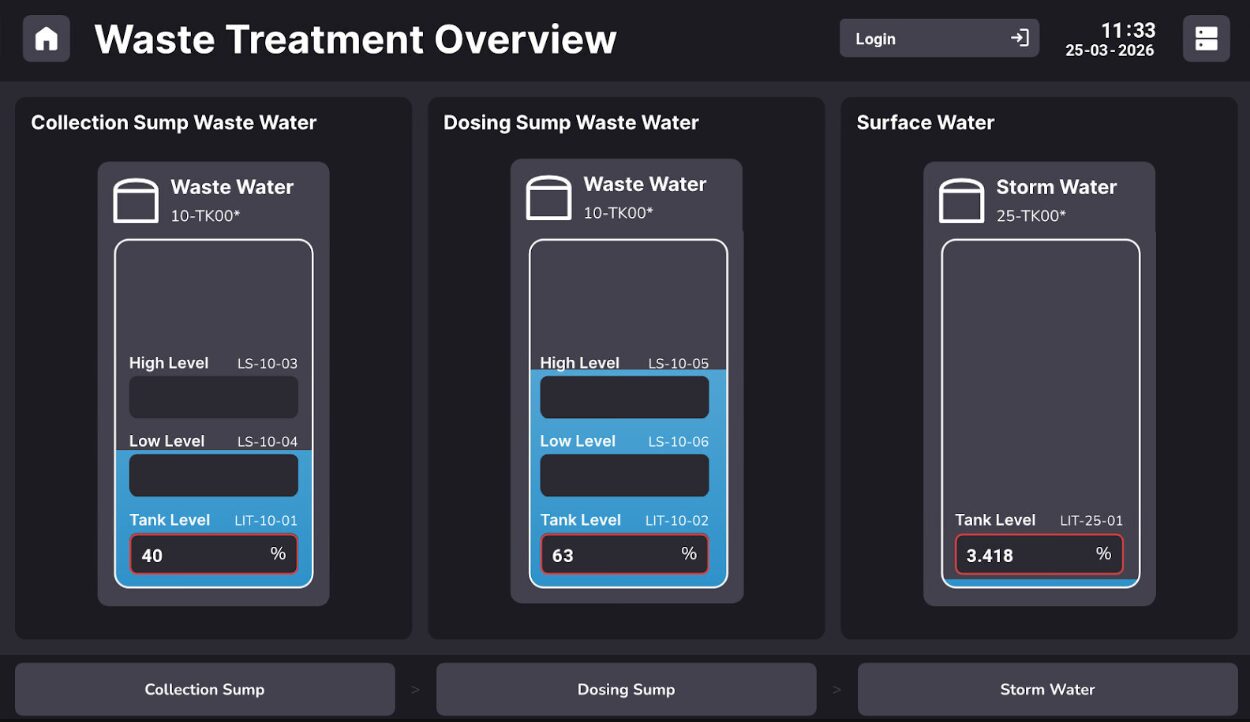
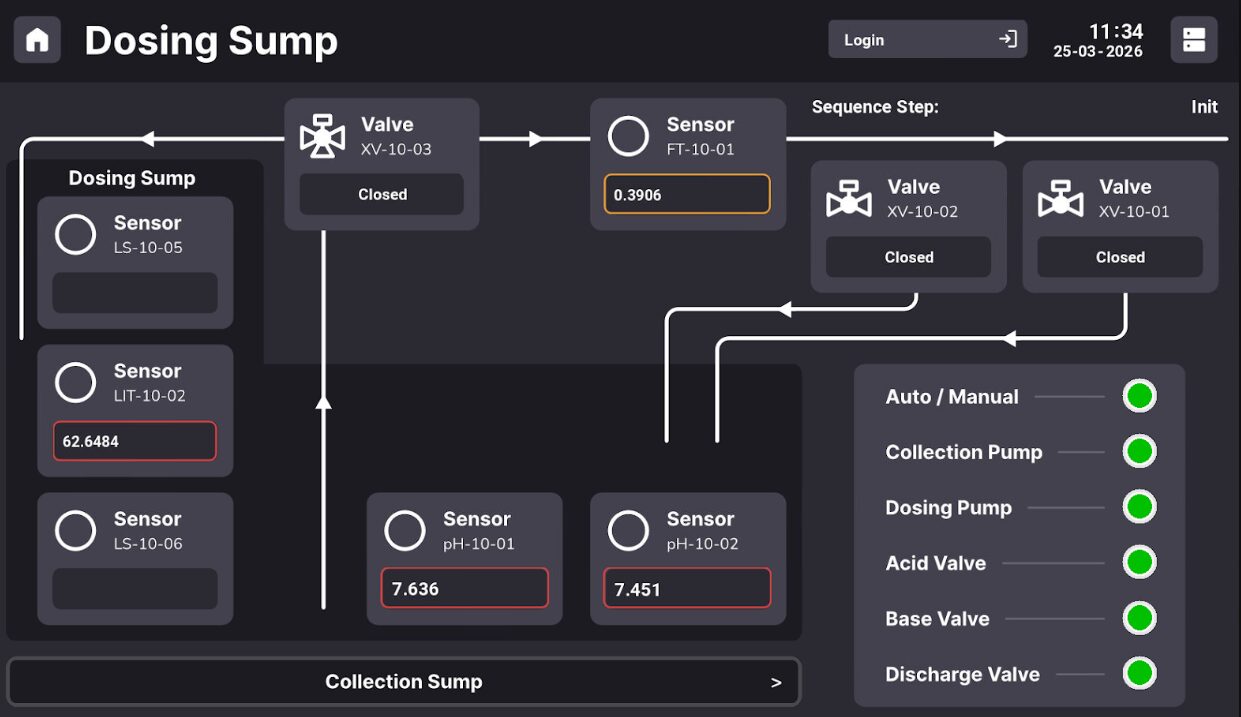
Automated Wastewater Monitoring & DosingBONNER delivered a wastewater monitoring and dosing system incorporating pH monitoring in the dosing sump and discharge line, flow and totaliser recording, level monitoring and pump interlocks. The system also provides closed-loop acid and caustic dosing from IBCs to help maintain discharge pH within required limits.
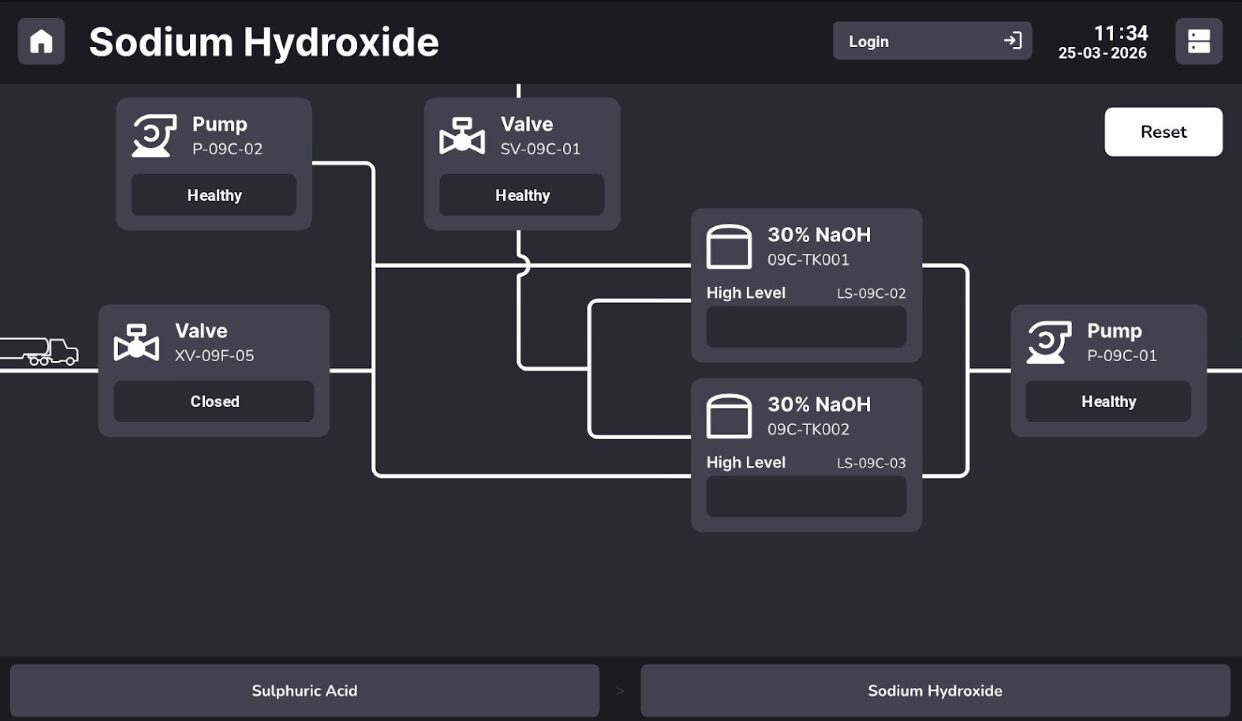
Plant-Wide SCADAAcross 2021 and 2022, BONNER implemented a plant-wide SCADA system using the B&R APROL platform.The system integrated existing site instrumentation to provide real-time monitoring, trending and reporting, giving site management a live view of plant status. Energy monitoring was also incorporated, providing visibility of consumption by zone and supporting more informed energy management.
Secure Remote Engineering AccessFor a site where a fully cabled network was not feasible, BONNER implemented secure remote engineering and support access using an industrially hardened VPN. This provides the engineering team with secure remote access while supporting faster response when technical assistance is required.
Functional SafetyBONNER also delivered functional safety projects to SIL requirements, including a tank unloading safety instrumented system. The work was supported by site risk assessment and documented safety design, ensuring the safety systems were developed around the specific risks and requirements of the site.
A key part of the partnership has been the way BONNER works alongside Carbon Group’s own engineering and maintenance teams. Each project has involved direct collaboration between the BONNER automation project team, Carbon Group’s site engineering and maintenance teams and its environmental monitoring team.
BONNER service and instrumentation technicians have also supported installation, calibration and commissioning. Direct communication between the BONNER project lead and Carbon Group’s site engineering management has helped keep projects aligned with the operational requirements of a live manufacturing environment.
SustainabilityEnergy monitoring was incorporated into the SCADA system to provide visibility of energy consumption across the plant by zone. This supports energy management in line with ISO 50001 and helps Carbon Group identify opportunities to target reductions.The automated wastewater dosing system also supports controlled and compliant discharge while enabling more efficient use of treatment chemicals.
Result
- Live visibility of plant status, supporting faster and better-informed operational decisions.
- Improved wastewater monitoring and dosing, supporting controlled and compliant discharge.
- Energy consumption visibility by zone, supporting more informed energy management.
- Enhanced safety, through SIL-rated functional safety projects.
- Secure remote engineering support, helping reduce response times and potential downtime.
- A connected automation approach, with further instrumentation and systems integrated into the existing SCADA environment.
- One long-term automation partner, supporting the site from concept and design through to commissioning and ongoing development.